


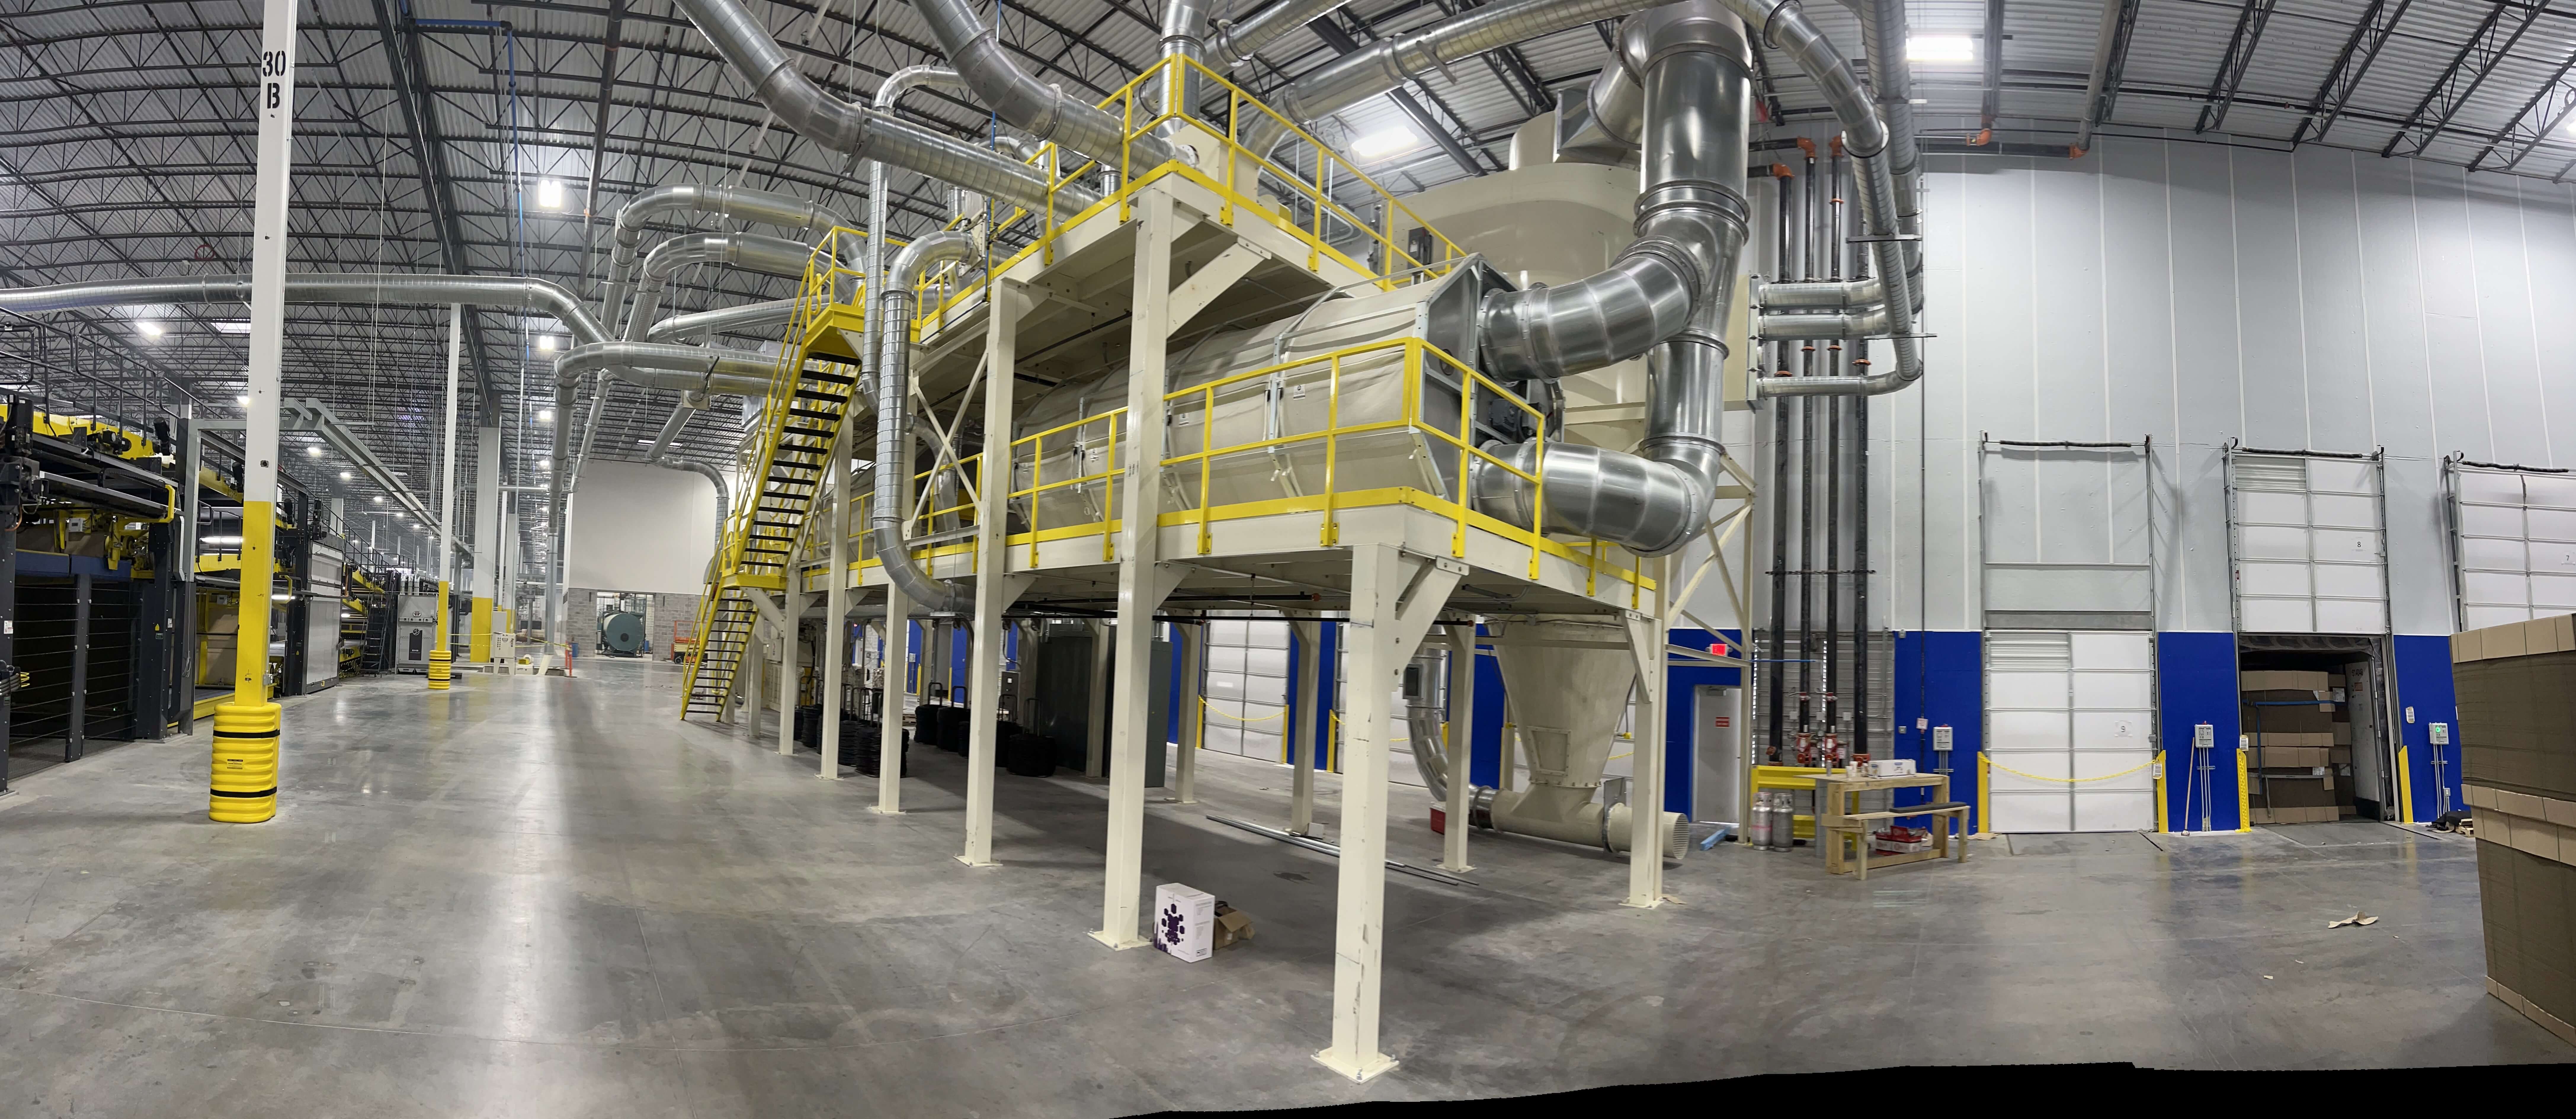

How ERS Builds a Dust Collection System
Industrial dust collection systems from ERS are engineered around the process that creates the dust, not bolted on after it. We size the hoods, the ducting, the separator and the filter as one system, for the air volume your plant actually moves and the material it actually makes.
Most of what we collect is fibrous and high-volume — paper trim, corrugated dust, tissue fly, wood, insulation, lightweight particulate. That material behaves nothing like metal fines, and a filter sized from a catalogue will blind within weeks. Ours are specified for the airflow and the dust in front of them.
A complete system has three stages. Capture at the machine, through hoods and pickup points placed where the material leaves the process. Transport, through ducting sized for the real velocity, which is what keeps material moving instead of settling in the duct. And separation and filtration, where the material drops out of the airstream and clean air goes back into the building rather than being exhausted and reheated.
For the separation stage we specify a cyclone separator where the dust is low in fibre and granular, and a low profile separator where headroom is the constraint — on a mezzanine, or under an existing roof where a conventional cyclone will not fit.
For the filter itself, continuous operations get the CCM® OCT filter. It cleans itself while it runs: the nozzles rotate and traverse across the full media on a single drive mounted outside the dust, so there is no cleaning cycle, no shutdown and no electrical component inside the drum. Media changes are tool-free and take minutes. Where combustible dust is in play, we also build explosion-proof filtration to match the hazard.
These systems run in corrugated plants, paper converting, tissue and hygiene, rotary die cutting and aluminum can production — and the same engineering sits behind our trim removal work, because in most plants the trim and the dust are one problem with one solution.
We survey the building first, measure the volumes and talk to the people running the machines. We fabricate, install around your production schedule, balance the system under real load and train your maintenance people before we leave. After that it stays ours to look after, with spare parts and field service out of Atlanta.
Bring your material to our test facility in Atlanta and we will run it before you commit.
What it costs to run
The question we get asked most is not what the system costs to buy, but what it costs to keep running — and the honest answer is that the two biggest numbers are air and media.
Air is the one most plants underestimate. Every cubic foot you exhaust is a cubic foot you have already paid to heat or cool, and it has to be replaced from outside. A system that returns filtered air to the building removes that penalty for most of the year. On a 40,000 cfm installation in a northern plant that is not a rounding error — it is the single largest operating saving the system makes, and it recurs every winter.
Filter media is the other. Media life depends almost entirely on how hard the filter is being asked to work, which is set by the design, not by the brand of fabric. A filter that is correctly sized and continuously cleaned runs for years; one that is undersized blinds, drives up fan power, and gets changed twice a season. That is why we size the filter to the airflow rather than to the price point.
Maintenance in year two should be unremarkable: a visual check of the nozzles, the scrapers and the media, and a differential pressure reading that tells you whether anything has changed. Nothing is replaced on a calendar. When media does need changing, it comes out by hand and goes back in the same shift.
And the cost nobody budgets for is downtime. A dust system that forces a production stop to clean itself costs more in lost output than it ever saves in capital.