


Briquette Press TH 800 M
The briquette press TH 800 M is the continuous-duty machine in the range, built for metal chips, swarf and turnings arriving steadily rather than in batches. It compacts them into dense briquettes and squeezes a large share of the cutting fluid back out on the way.
What it is for
Machining waste is awkward in its loose form. Turnings tangle, take up a great deal of space for very little weight, and carry coolant with them wherever they go — into the skip, onto the truck, and off site with the scrap. Compacting them changes all three.
The briquette that comes out is dense, dry enough to handle and stackable. No binder is used; it holds together on compaction alone.
Coolant recovery is usually the argument
On a wet machining stream the fluid pressed out of the chips is collected rather than carried away. Over a year that is a quantity worth measuring, and on many sites it is the single number that makes the case for the press before anything else is counted.
It also changes what the scrap is worth. A dry, dense briquette is a cleaner product to a buyer than a drum of wet turnings, and it is weighed as metal rather than as metal plus fluid.
Sizing and duty
The TH 800 M sits above the C 150 and C 170e and the TH-Series, and below the TH 1500 M. The full range is set out on the briquette press page.
Choosing between them is a question of how much material arrives per hour and how consistently, not of which machine has the highest figure on paper. A press sized for a peak that happens twice a week spends the rest of its life running below its design point, and one sized for the average stalls when the shop is busy.
What feeds it well
Consistency matters more than volume. A feed that is reasonably uniform in size compacts predictably; one that swings between fine grindings and long stringy turnings produces briquettes that vary in density. Where a stream is mixed, size reduction upstream through a shredder evens it out before the press sees it.
Tramp metal is the other thing to design out. A bolt or an offcut traveling with the chips reaches the auger eventually, so on mixed streams ERS puts magnetic separation ahead of the press rather than relying on somebody spotting it.
How it is fed
Hand-loading a hopper caps the line at whatever a person can lift, which is the wrong constraint on a machine built for continuous duty. ERS builds the conveying in from the start, so the press is fed at a steady rate rather than in surges.
Where the chips are collected pneumatically, the press sits under the cyclone at the end of the dust collection system and takes the discharge directly.
Options worth specifying
A level sensor, hydraulic oil heating and cooling, and automatic length adjustment are all available. Oil heating earns its place in an unheated building, because cold oil changes how the press behaves on the first cycles of a shift.
Automatic length adjustment is worth having wherever the briquettes go into a container or onto a conveyor and a consistent size makes the handling predictable.
Maintenance and wear
The wear parts are where the material does the work: the auger, the pressing chamber and the die. Metal-bearing feedstock is abrasive, so these are consumables rather than fit-and-forget components, and their life depends heavily on what is being pressed.
Access is the practical point. A press installed hard against a wall under a cyclone takes twice as long to service, so ERS plans the position for the maintenance as well as for the duct run. Wear parts are held and supplied from Atlanta.
What changes on the shop floor
The visible change is space. Loose turnings fill a skip quickly and have to be moved before they are anywhere near a full load, so a shop ends up paying for hauls that are mostly air. Briquettes go into the same container at a fraction of the volume, which cuts the number of collections as much as the weight.
The less visible change is handling. Loose chips sit in open containers around the machines, get walked through, and end up on the floor between the lathe and the skip. A press at the end of the collection system turns that into a single predictable output at one point in the building.
Where it sits in the plant
A briquette press is the discharge end of something larger, which is why ERS specifies it alongside the collection and conveying it depends on as part of metals processing rather than as a machine bought on its own.
How a project starts
With the material and the numbers: what the stream is, how much arrives per hour, how wet it is, and where the briquettes and the recovered fluid need to end up. Material can be run at the ERS test facility in Atlanta when a question is better settled than estimated.
Every system ERS supplies is installed, commissioned and supported by ERS, with spare parts and service from Atlanta. Talk to ERS about your chip volumes and your coolant.
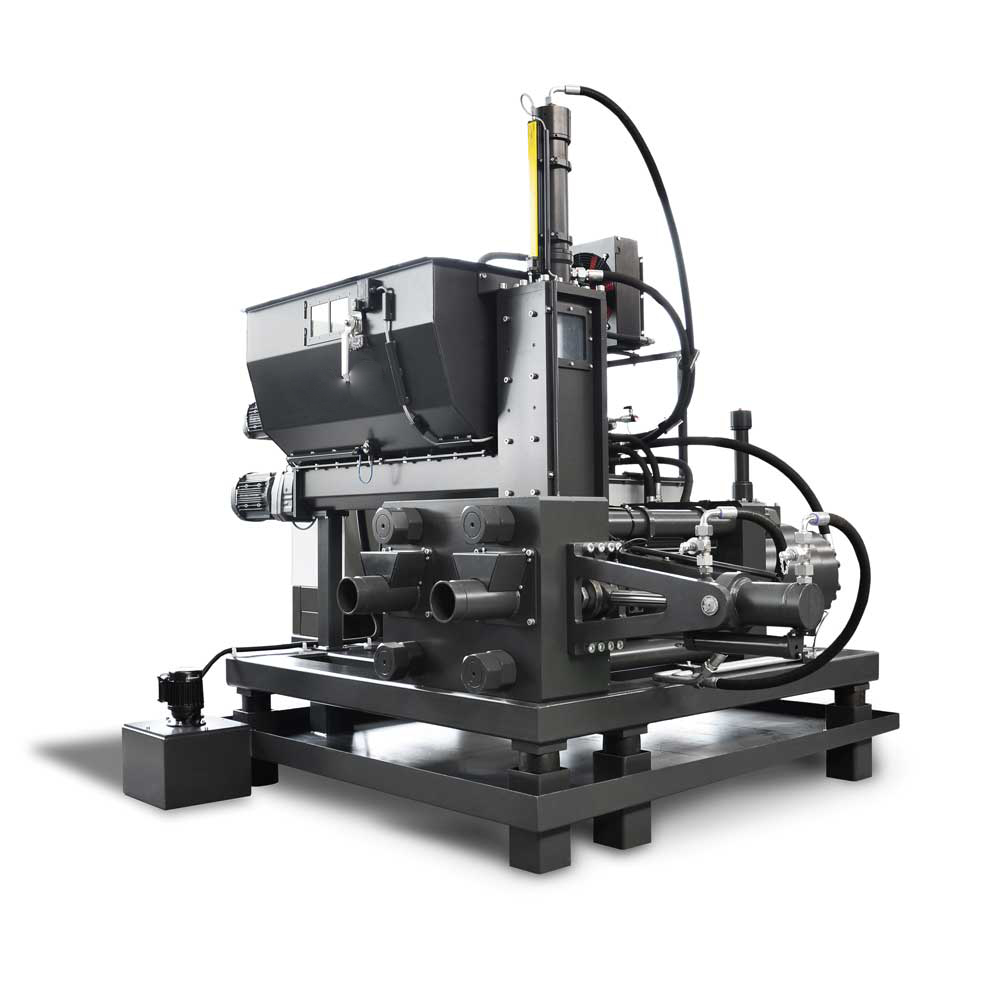
Technical Data WP 600 + TH 800 M
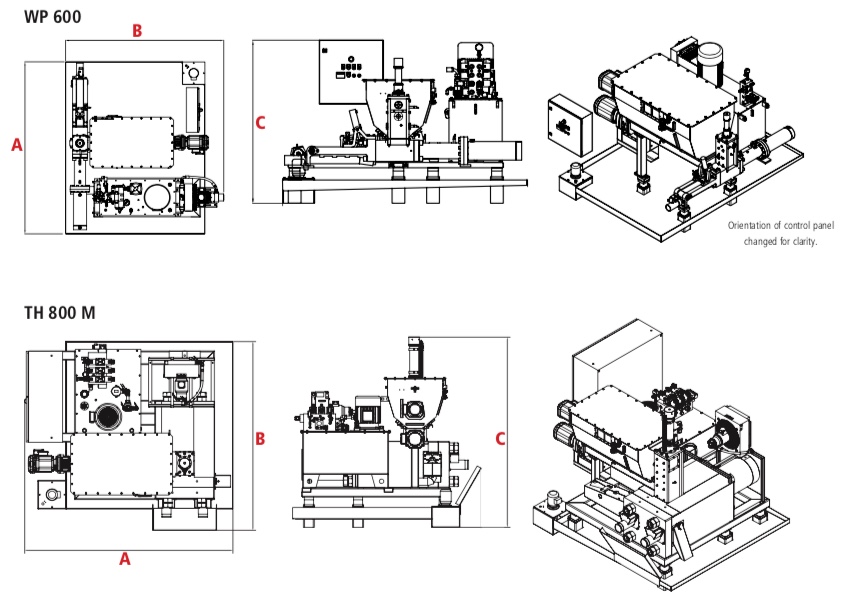
| WP 600 | TH 800 M | |
|---|---|---|
| Dimensions C | 61.25" (1,533 mm) | 82" (2,088 mm) |
| Briquette Diameter | 2.4" (60 mm) | 3.2" (80 mm) |
| Hydraulic oil quantity | 42 g (160 L) | 66 g (250 L) |
| Hydraulic motor | 12 hp (9 kW) | 16 hp (22 kW) |
| Weight | 2,205 lbs (1,000 kg) | 6,600 lbs (3,000 kg) |
| Dimensions A | 90" (2,300 mm) | 90" (2,300 mm) |
| Dimensions B | 83.5" (2,118 mm) | 81" (2,069 mm) |