Pre-Shredder
Guidetti
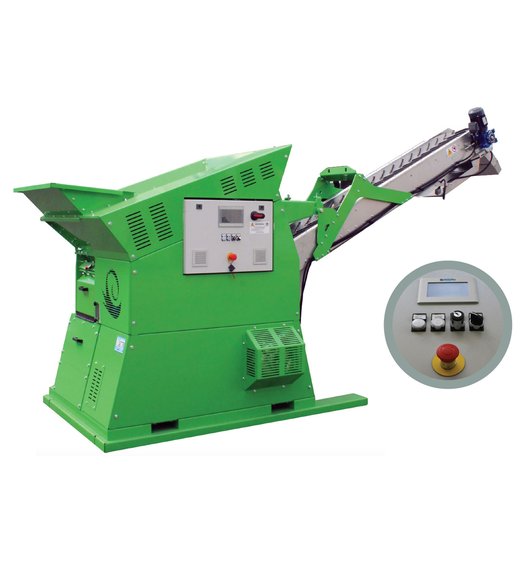
PMG 400
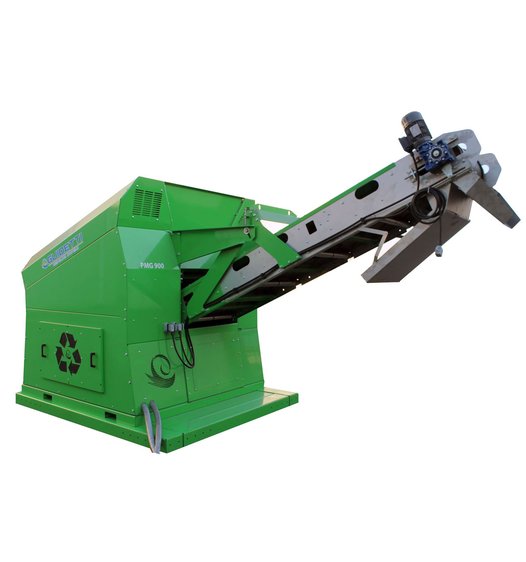
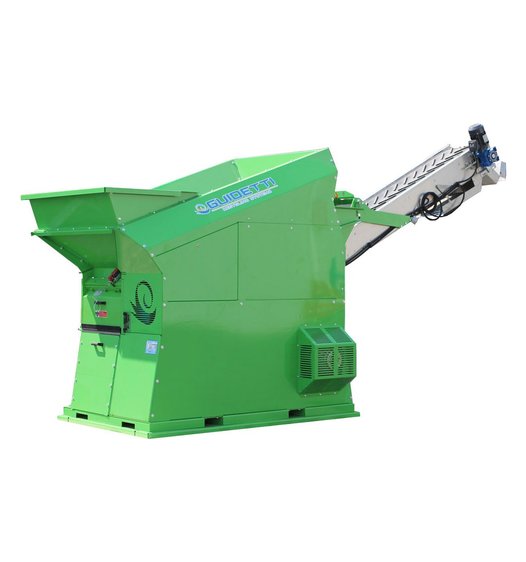
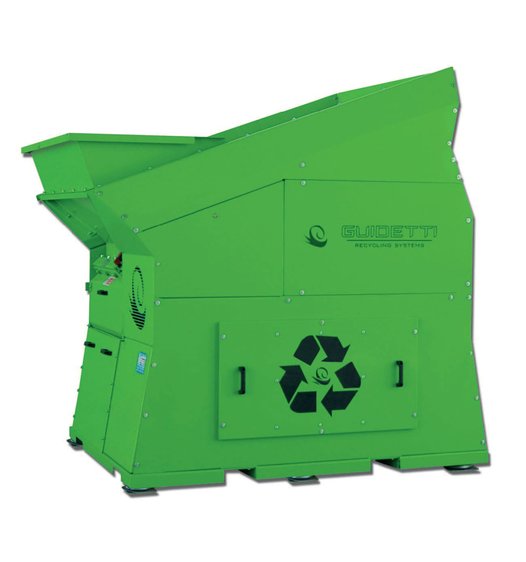
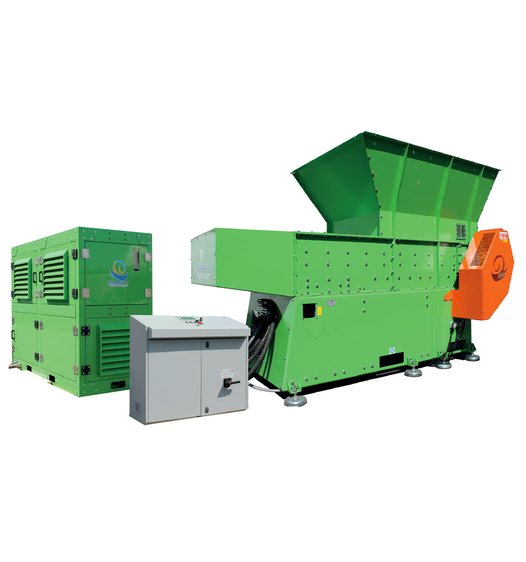
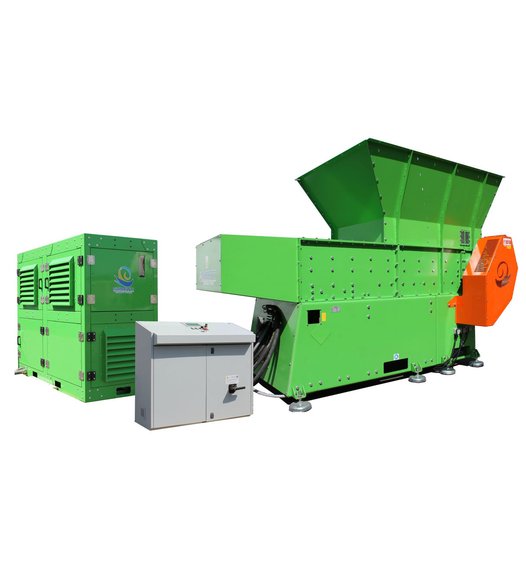
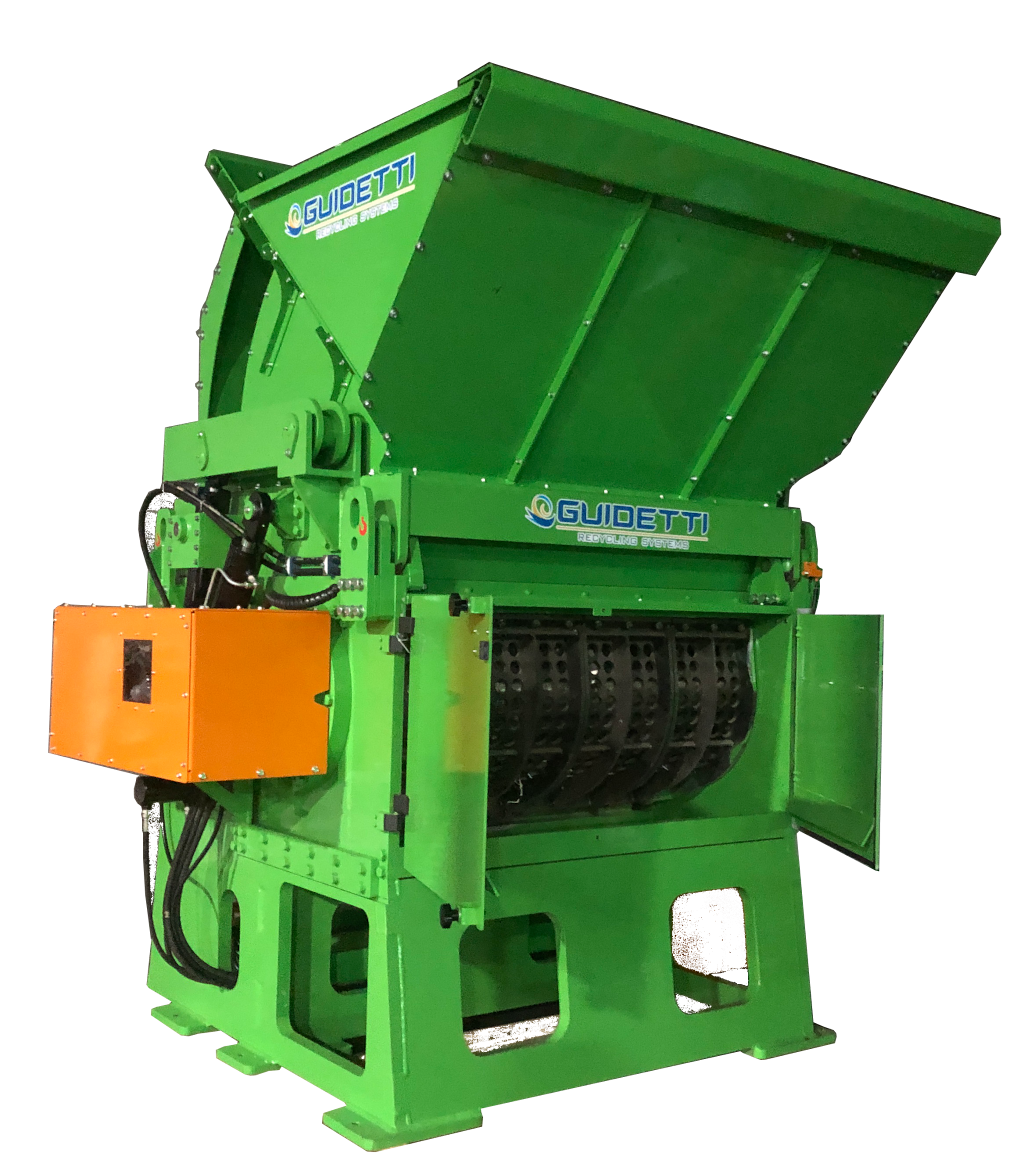
PMG 900 H Hydraulic Pre-Shredder for Cable and Metals
The Guidetti PMG 900 H pre-shredder is the entry point to the hydraulic end of the PMG range. It is a single-shaft machine built for feed that stalls an electromechanical drive — armored and bundled cable, dense non-ferrous scrap, composites and reinforced industrial waste — and it is CE certified. Engineered Recycling Systems supplies, installs and supports it from Atlanta.
What the H means
Guidetti builds the PMG range in two drive types. The PMG 400 and PMG 600 are electromechanical. The 900 H, 1200 H and 1600 H are hydraulic.
A hydraulic drive holds torque at low speed instead of tripping, so material that jams an electromechanical machine keeps moving through this one. The 900 H is where that capability starts: below it there is no hydraulic option, so a plant with genuinely difficult feed and modest volume still begins here rather than smaller.
Installed power
52 HP (38.5 kW). That is the figure for this machine, and it is worth stating plainly because the larger hydraulic models are often quoted alongside it — the 1200 H runs a 105 HP (78 kW) control unit and the 1600 H a 177 HP (132 kW) one. Those belong to those machines, not to this one.
The weight is 6,260 lb (2,840 kg) and the footprint 83 x 81 x 88 inches (2110 x 2070 x 2245 mm), which is what usually decides whether it goes where a plant wants it.
Throughput, honestly
Guidetti publishes a capacity range for the PMG series rather than a figure per model, because production depends on installed power, screen size and the material itself. Anyone quoting a single number for a specific machine is quoting the series.
Clean cable and mixed contaminated scrap will not run at the same rate through the same rotor. The number worth planning around is the sustained one on the plant's own material, which comes from a trial.
Single-shaft, and why it matters
The PMG series is single-shaft. Material is fed manually or by conveyor into the cutting chamber, where the rotor fragments it at low speed against the screen.
Low speed keeps dust and noise down and gives a uniform particle size, which matters far more than raw speed when a granulator is waiting behind it.
Taking the ferrous out
A conveyor belt with magnetic pulley carries the output away and pulls ferrous contamination out inline. Overband separators are available in several sizes where the ferrous load justifies one, and the wider magnetic separation range covers the rest.
Taking that metal out before the next machine is cheaper than taking the next machine apart.
What it feeds
The pre-shredder is stage one. Behind it sit Sincro granulation lines for cable, dry separation tables for the density split, and hammer mills where final sizing is needed.
Protecting those stages is most of the economic case. A granulator fed oversized material jams, wears fast and gives an inconsistent fragment. Fed a sized feed it runs at its rated throughput and its knives last, so the saving shows up in wear parts rather than in headline tonnage.
What runs through it
Copper and aluminum cable, including constructions a lighter machine will not take. Rubber, plastics, paper and composite scrap. E-waste too bulky to go straight into a precision machine, and mixed industrial feedstock that arrives in whatever shape the last process left it.
The common factor is resistance rather than material type. If it is too tough, too dense or too tangled for the next machine, it goes through a pre-shredder first — and if it is tough enough to stall one, it goes through a hydraulic one.
Where it fits in a line
ERS integrates the 900 H with conveyors, granulators, air separation and dust extraction so the stages balance. A pre-shredder that outruns the granulation behind it does not raise output, it just moves the bottleneck somewhere harder to see.
Feed and discharge usually decide the real throughput. Material arriving in surges, or a discharge that backs up, costs more over a year than the difference between two machine sizes.
Maintenance
Easy-access panels and a rotary valve system keep material moving and make inspection straightforward. Sealed bearings, reinforced housings and an operator-level control interface suit continuous duty with minimal supervision.
The hydraulic system adds its own routine — fluid condition, filters and hose inspection — and it is light work compared with what a stalled drive costs in a line that has to keep running. ERS sets the schedule out at commissioning so it lands with the rest of the plant's maintenance, not on top of it.
Blades and screens are consumables. What decides their real cost is how long the line stands still while they are changed, which is why access is designed in rather than worked around.
How a project starts
With the material. ERS looks at what arrives, in what volume, what has to be recovered and the building it has to fit inside. Material can be run at the ERS test facility in Atlanta before anything is specified, which on a hydraulic machine is worth doing properly — the drive is chosen off the worst feed, not the typical feed.
Every machine ERS supplies is installed, commissioned and supported by ERS, with spare parts and service from Atlanta. The full Guidetti range sits alongside the rest of the ERS metals processing equipment.
Talk to ERS about what you are feeding and what the next machine needs to see.